Explore our premium range of high-performance luggage, anti-theft messenger bags, customizable totes, and business briefcases manufactured under strict ISO9001 standards.


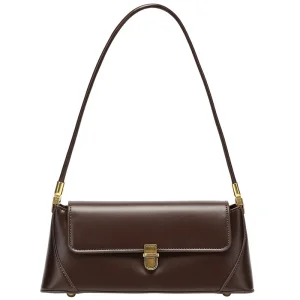
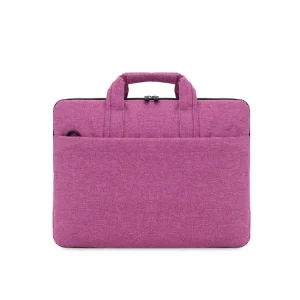
Understanding the dynamic shift in global luggage procurement, material technology, and China’s dominant manufacturing hubs.
The global travel bag and rolling luggage market is experiencing unprecedented demand, projected to exceed USD 45 Billion by 2030 at a CAGR of 6.8%. Driven by expanding international business travel, digital nomadism, and corporate mobility, enterprise buyers are prioritizing lightweight, highly resilient, and multi-functional rolling luggage solutions.
Modern commercial procurement demands products that combine structural integrity—such as aviation-grade aluminum telescopic handles and omnidirectional dual-spinner wheels—with refined aesthetics suitable for executive environments.
China remains the undisputed epicenter of global luggage manufacturing, accounting for over 70% of worldwide production capacity. The key to this dominance lies in specialized regional clusters such as Baigou Town, Hebei Province—recognized globally as the "Luggage Capital of China."
Industrial clustering allows premier manufacturers to maintain localized supply chains where raw fabrics, high-durability zippers, custom hardware, and ergonomic trolley assemblies are sourced within a 15-minute radius, dramatically compressing production lead times.
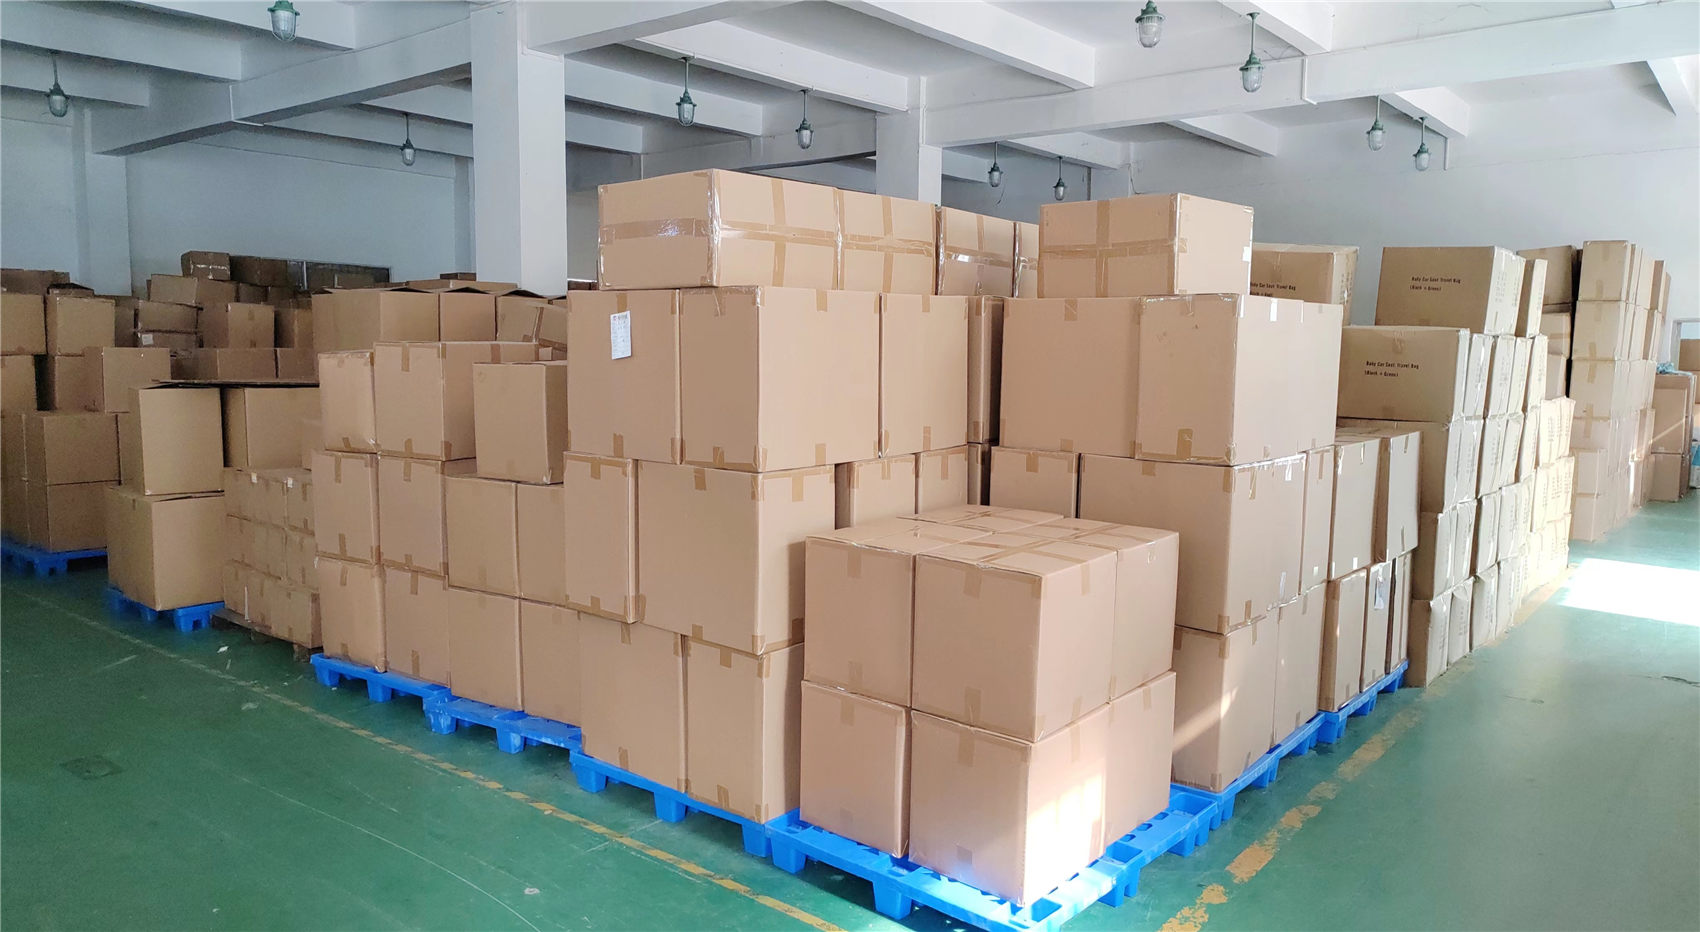
A flagship manufacturing plant operating in the heart of China’s luggage production ecosystem.
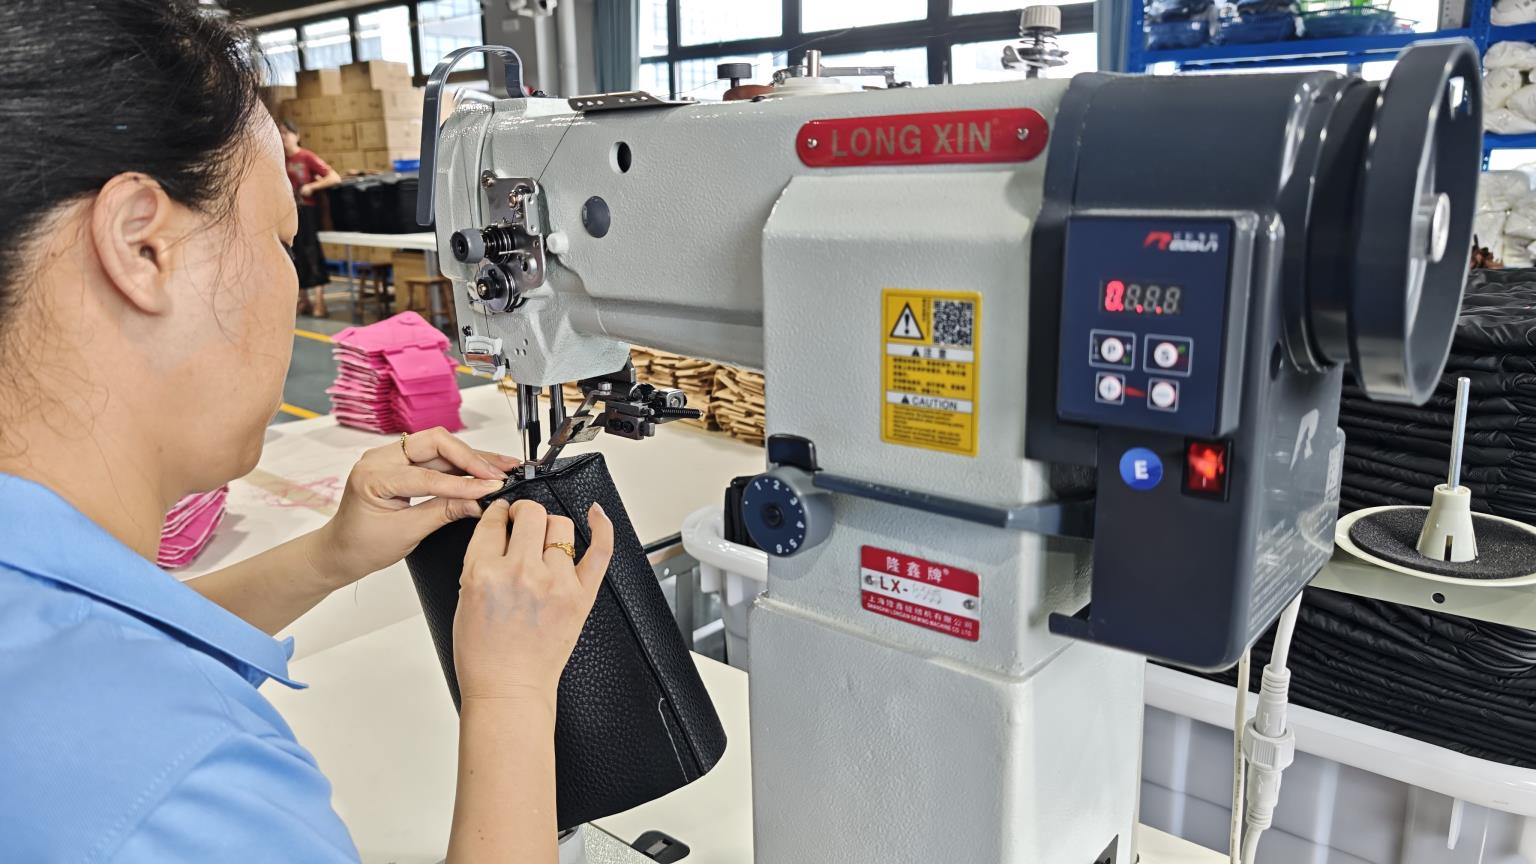
Established in 2009, Hebei Ripped Fashion Co., Ltd. is strategically located in Baigou Town, Baoding City, Hebei Province—widely celebrated as the primary "luggage capital of China." By directly leveraging its robust local supply chain advantages and mature industrial ecosystem, the company has evolved into a premier OEM and ODM manufacturer specializing in heavy-duty rolling bags, fashion luggage, business briefcases, backpacks, and promotional tote solutions.
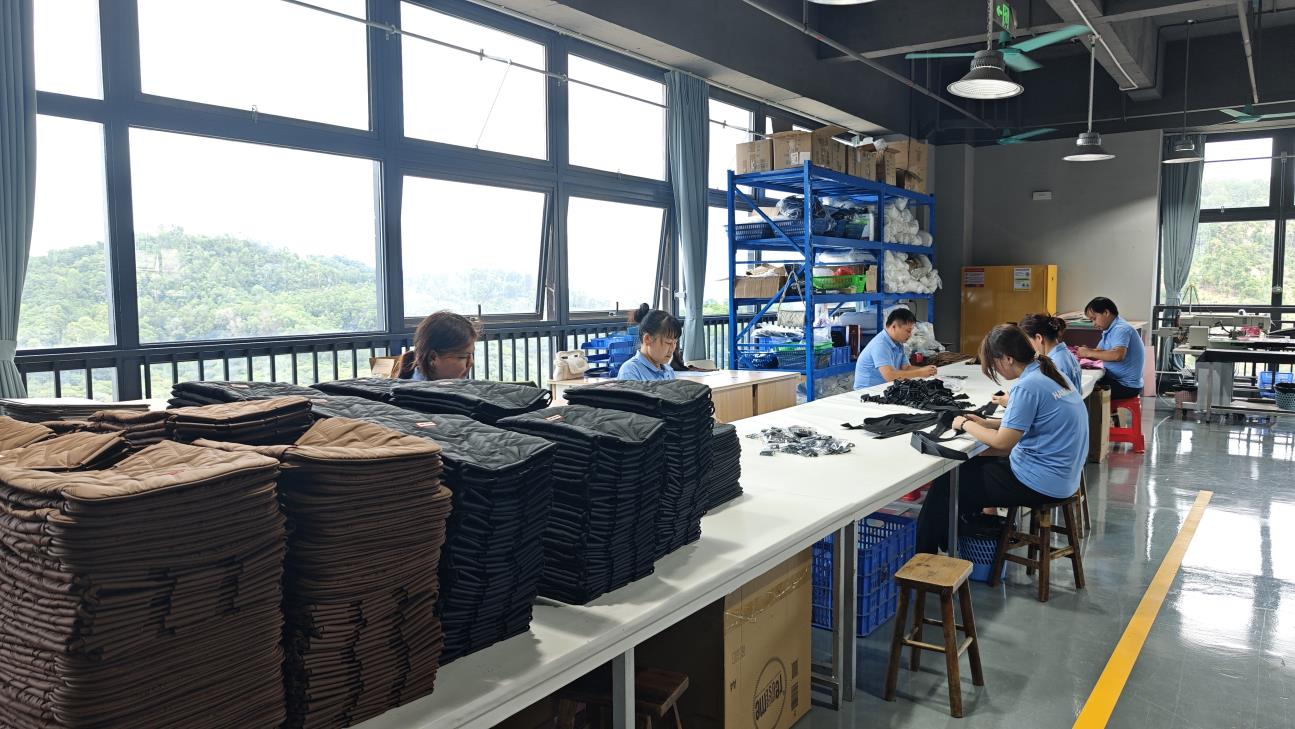
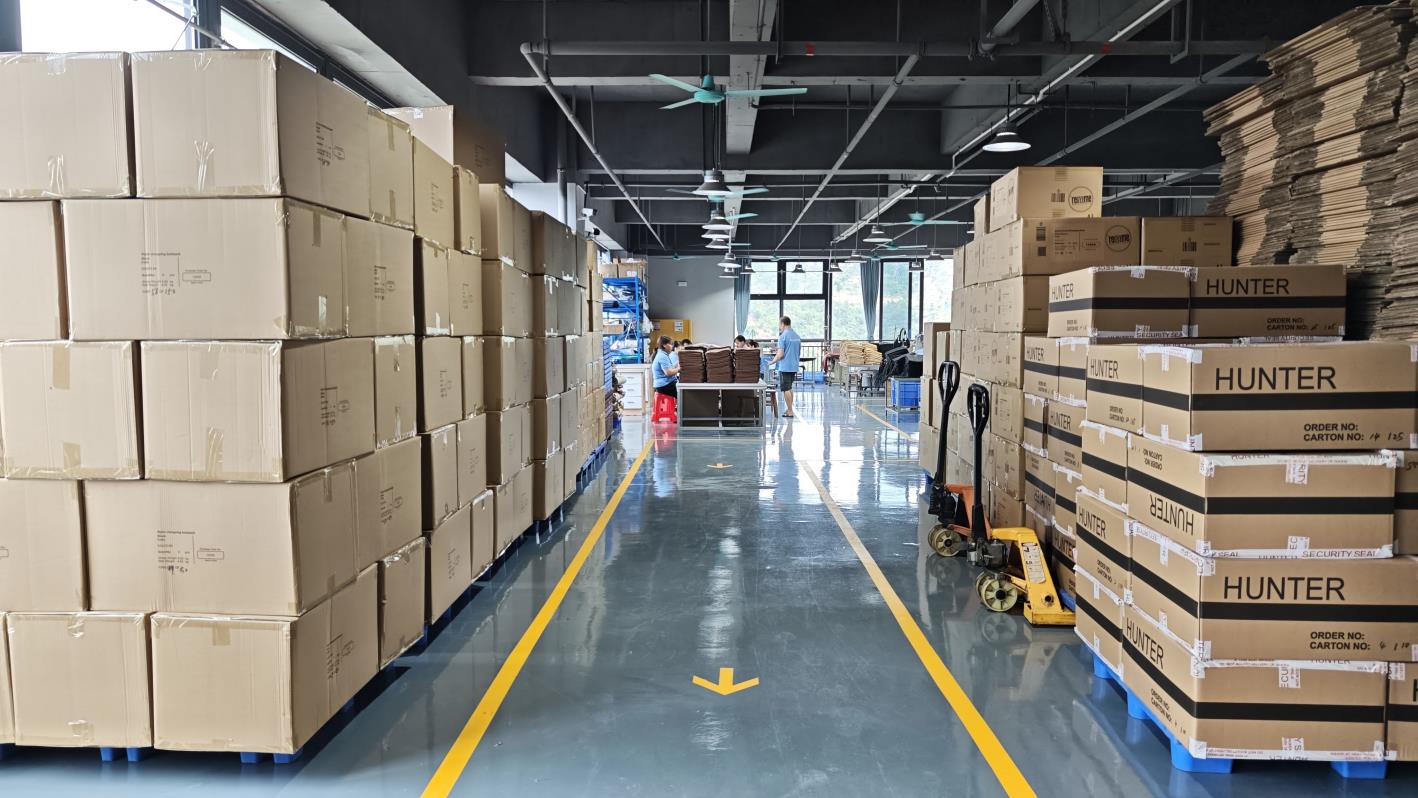
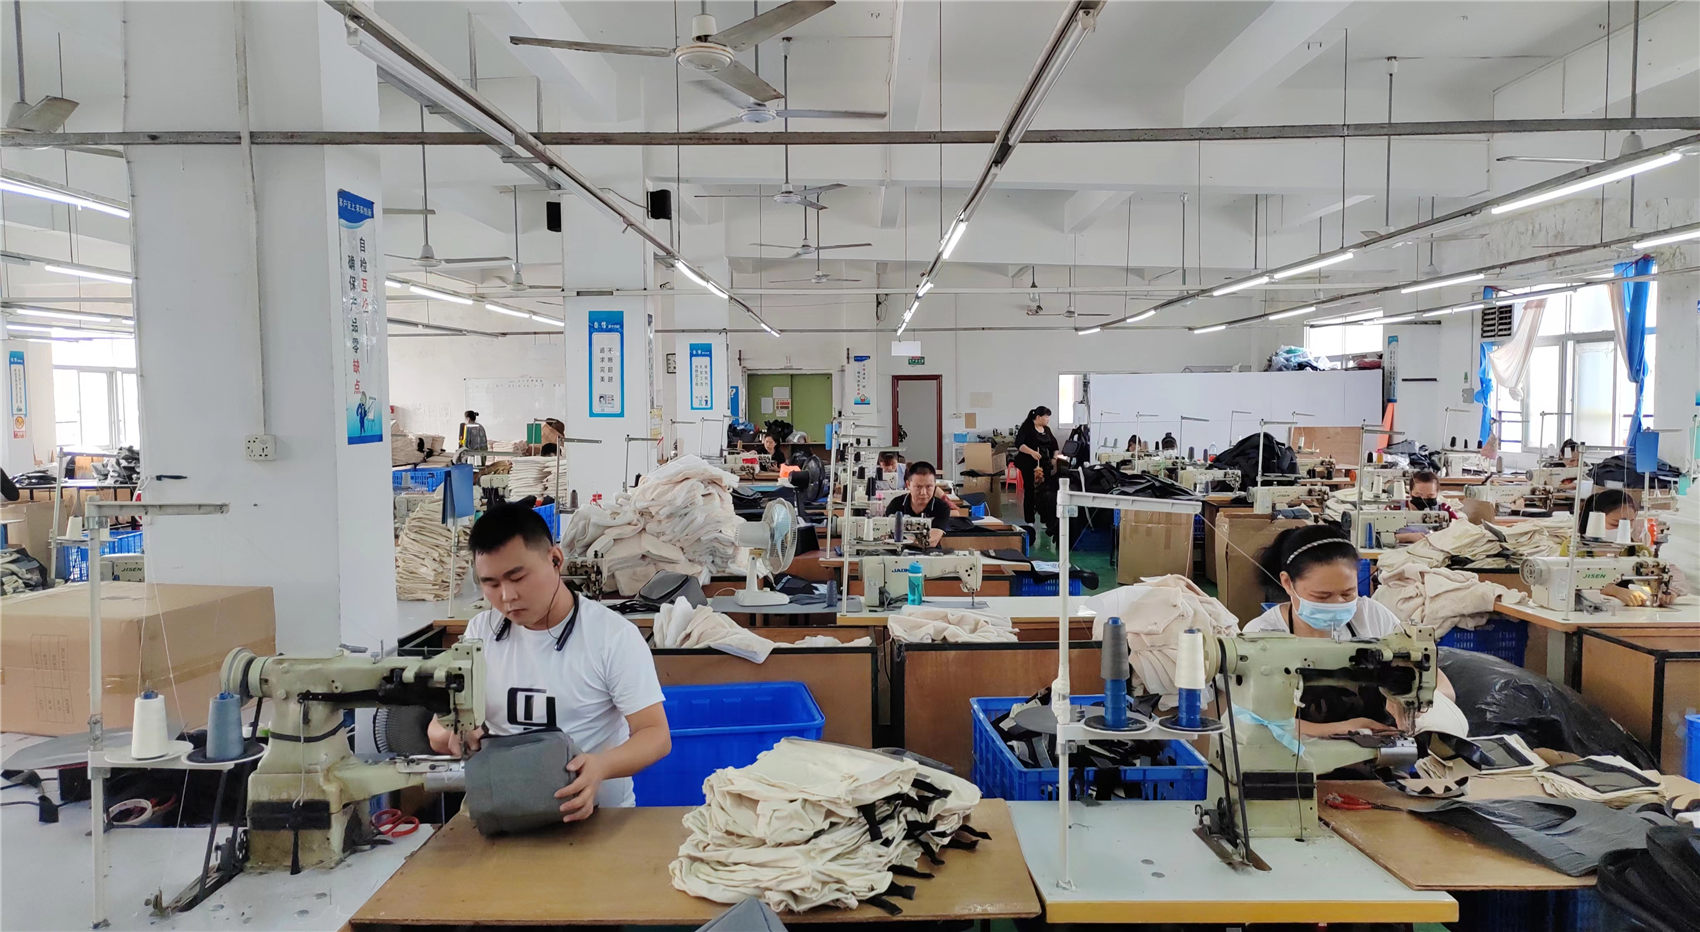
Occupying a total facility area of approximately 3,000 square meters, including a dedicated 2,000-square-meter modern production workshop, the plant operates with a highly skilled workforce of over 300 experienced craftsmen. Guided by the core operational principles of uncompromising quality control, direct factory price efficiency, and rapid turnaround schedules, the company maintains long-standing B2B partnerships across North America, Europe, Southeast Asia, and the Middle East.
With over 20 years of combined technical experience across its executive engineering and design teams, Hebei Ripped Fashion Co., Ltd. continually updates its portfolio to integrate emerging functional trends—ranging from TSA-approved anti-theft locking systems and integrated USB charging ports to eco-friendly rPET fabrics and ultra-silent polyurethane spinner wheels.
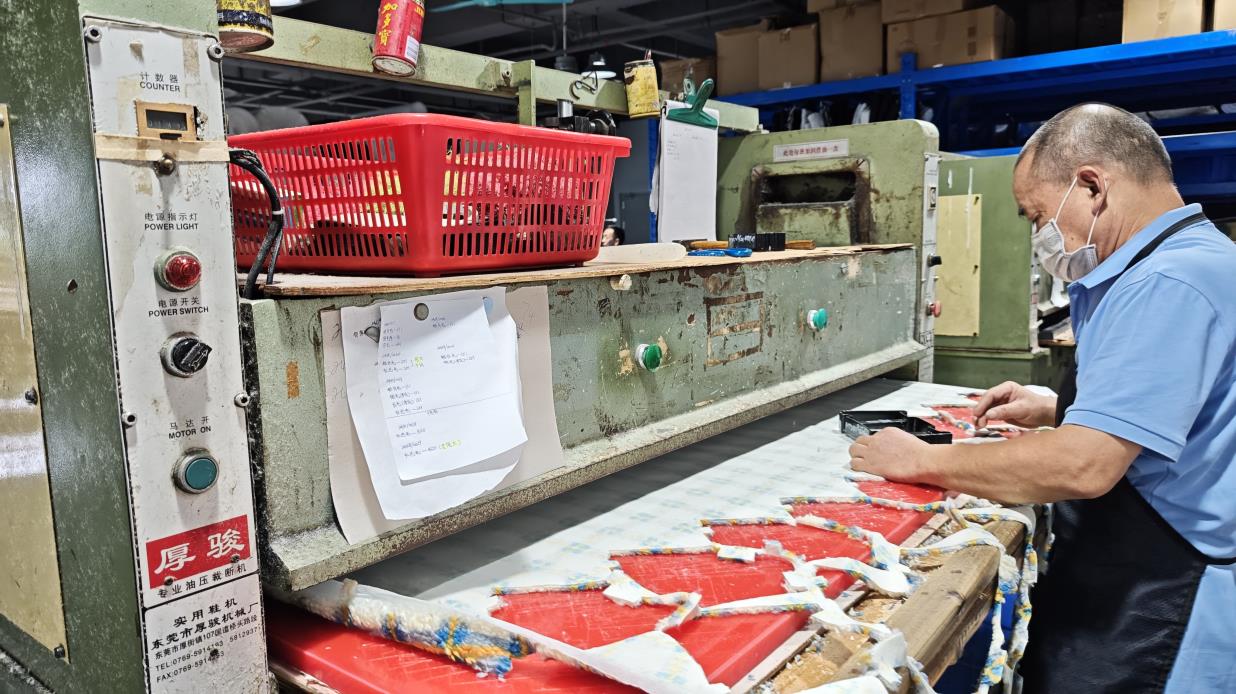
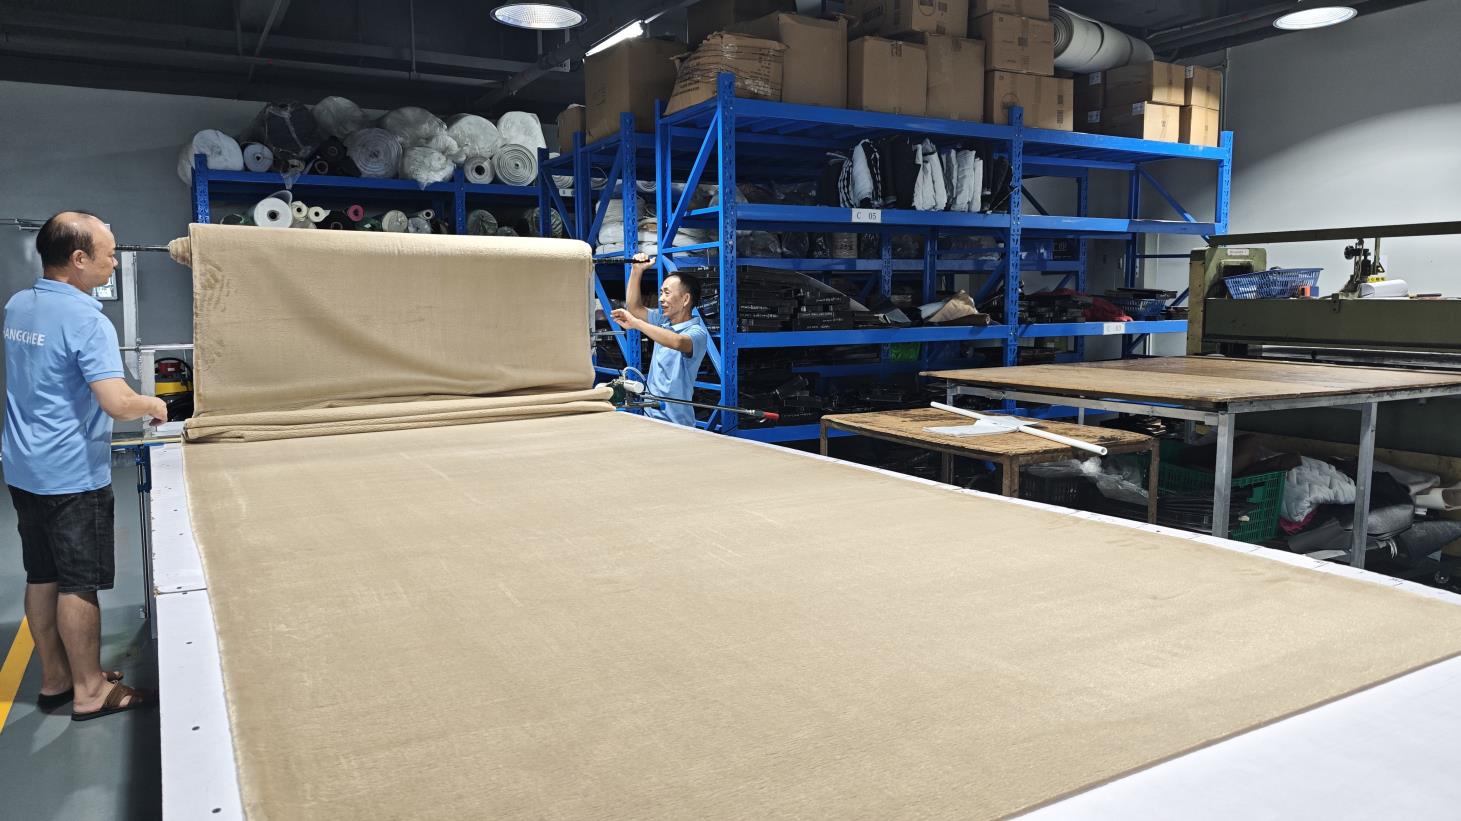
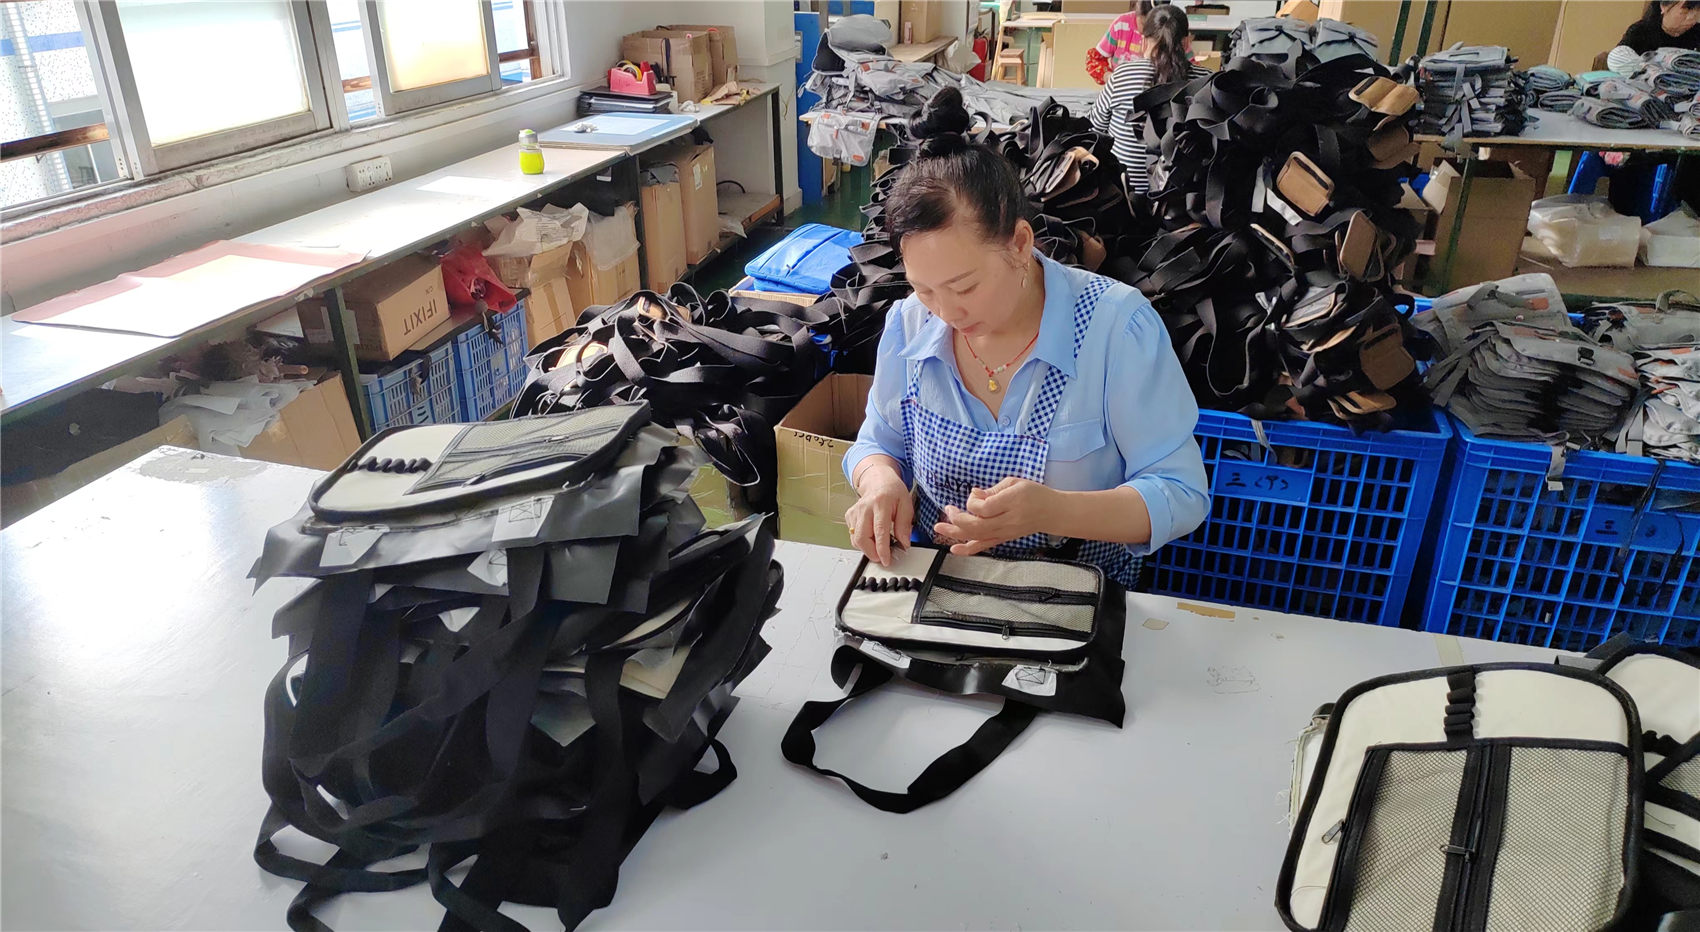
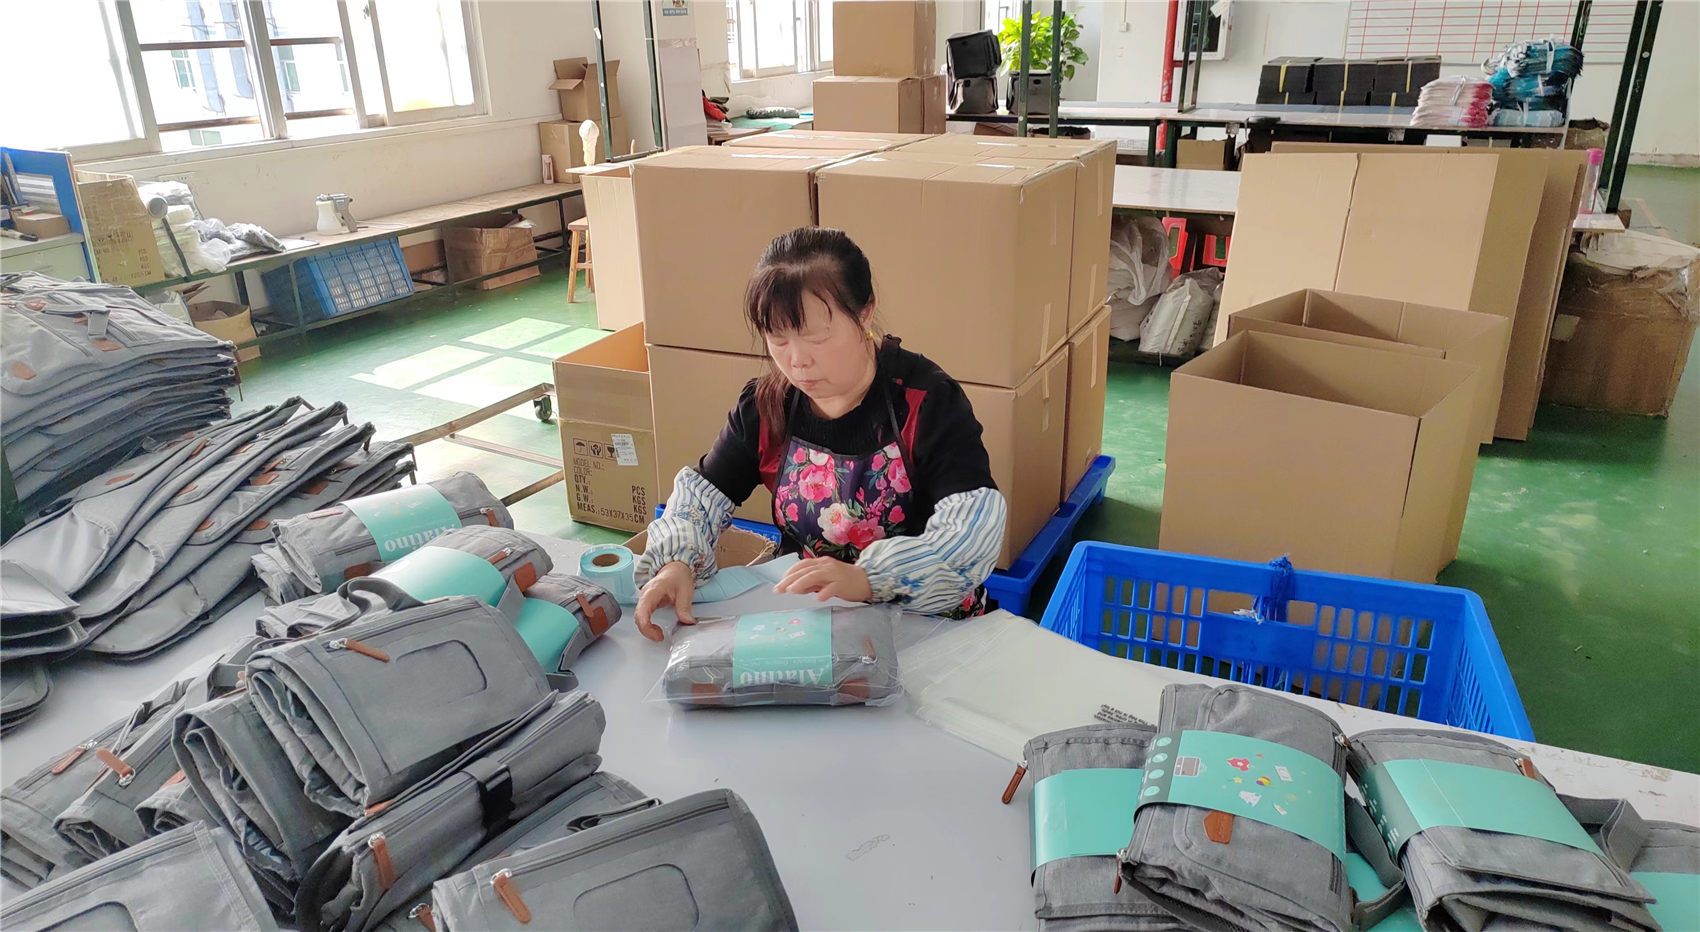
Transparent visualization of our standardized Industry 4.0 manufacturing workflow.
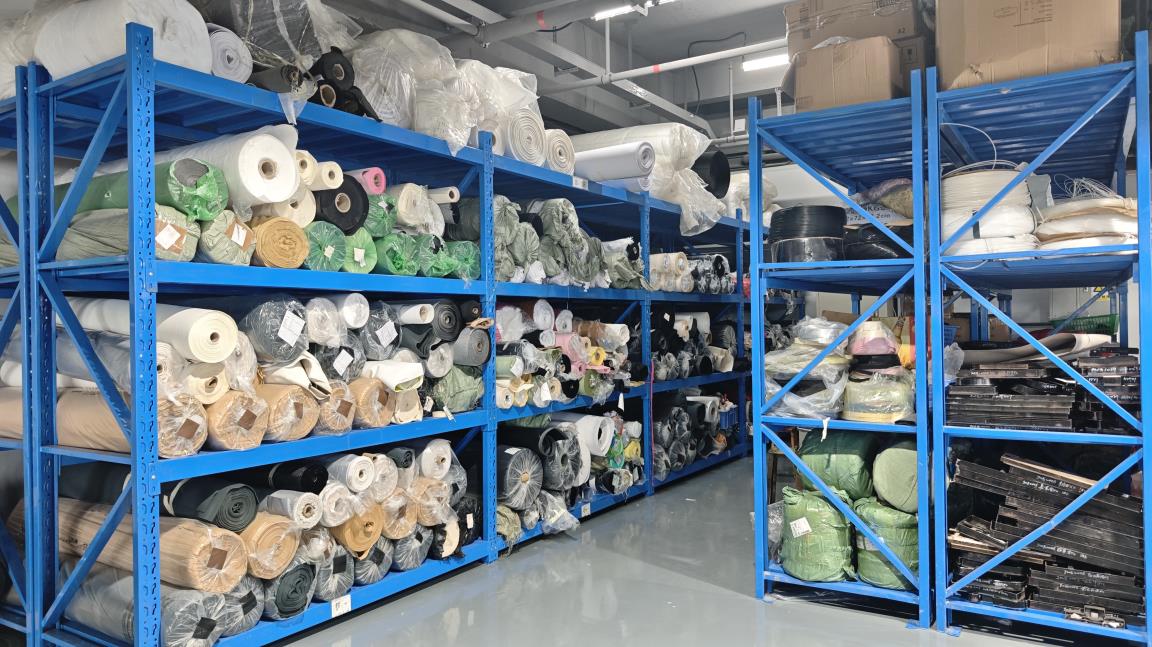
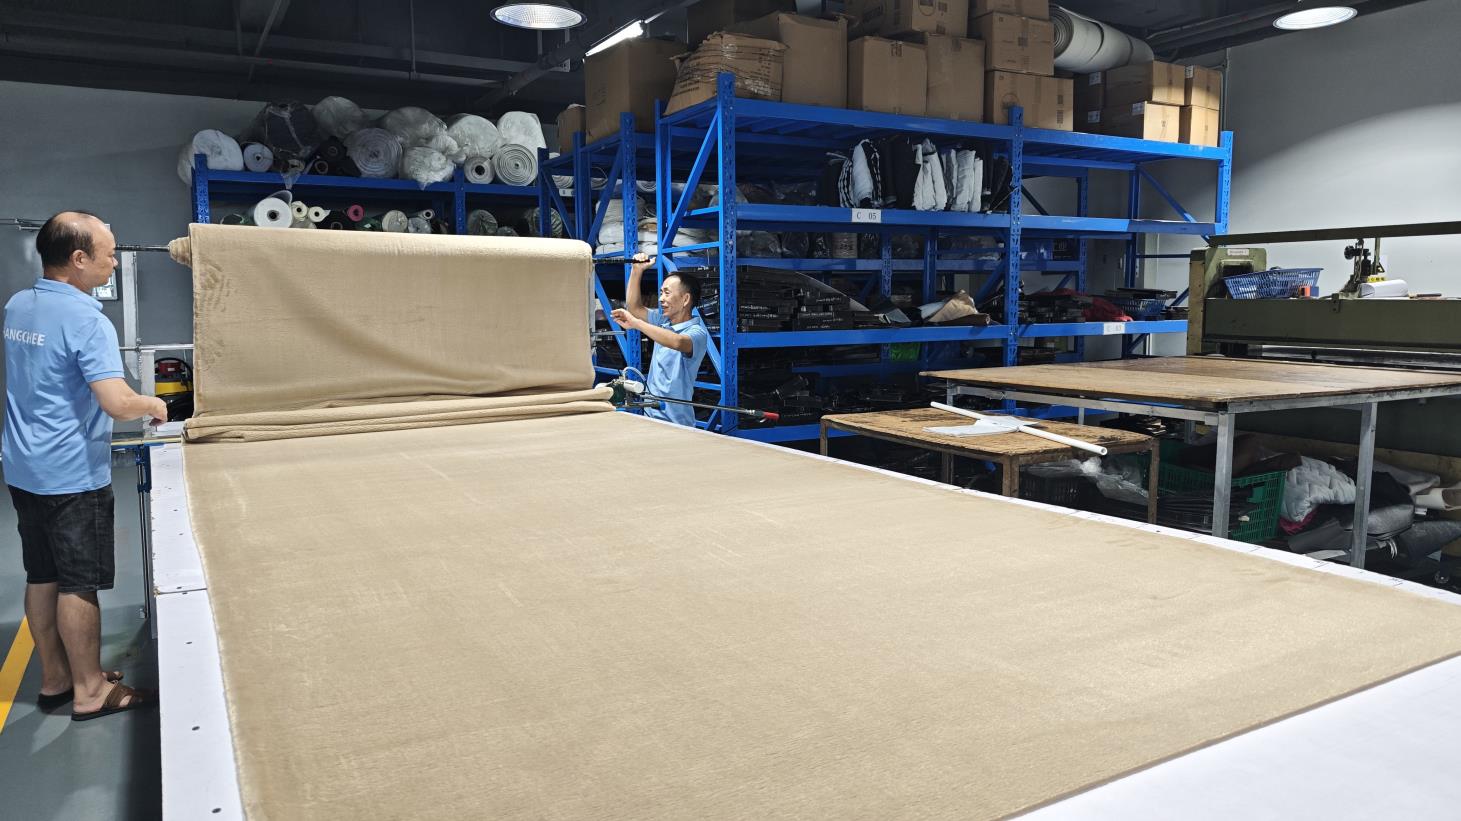
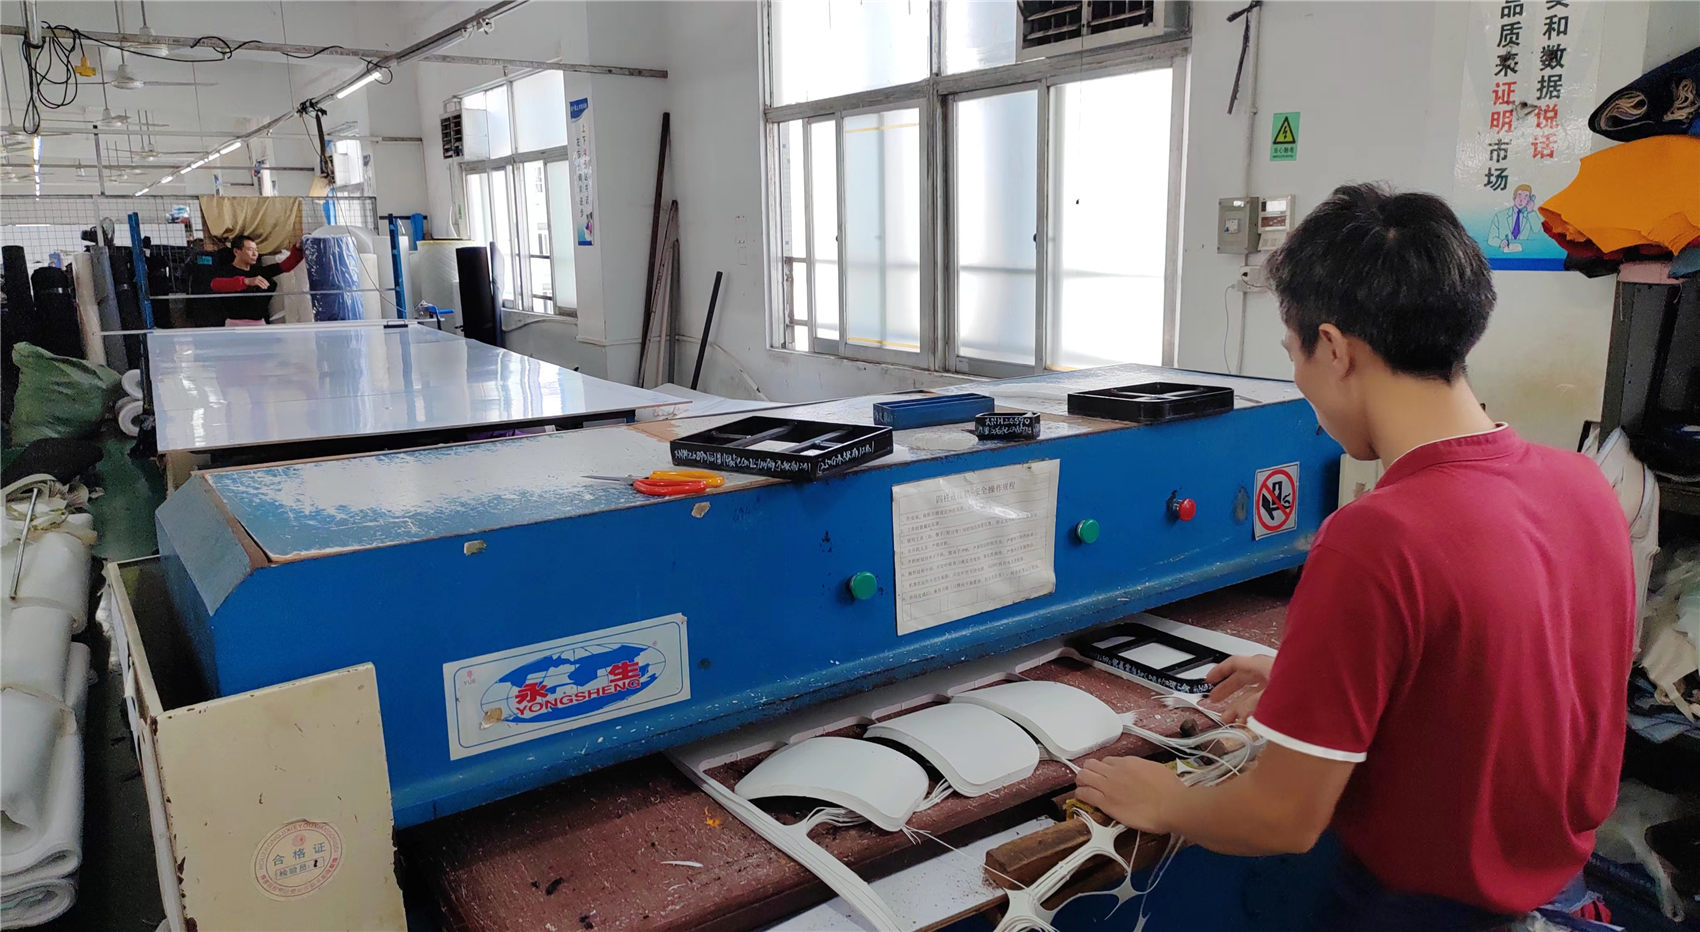
How digital integration, automated machinery, and localized clusters lower unit costs while guaranteeing institutional quality.
By implementing computer-controlled CNC fabric laser cutters and automated pattern nesting software, China’s top rolling bag manufacturers minimize raw material waste by up to 18%. This technological precision guarantees that every panel cut for softside luggage or hard shell poly-carbonate lining adheres strictly to millimeter-level tolerances.
Factory-floor digitalization allows real-time tracking of defects during stitching, trolley assembly, zipper endurance testing, and wheel impact resistance evaluations. Dynamic testing includes handle jerk testing (over 5,000 cycles at full payload) and drop testing from heights up to 1.5 meters under frozen conditions.
Proximity to Tianjin Port and Beijing Daxing International Airport provides unmatched export elasticity. Supply chain buffers ensure raw materials like 1680D Ballistic Nylon, 600D Cordura, high-grade aluminum rods, and heavy-duty YKK zippers are restocked within 24 hours, ensuring uninterrupted production schedules.
Deconstructing what corporate buyers, private label brands, and chain distributors look for when selecting rolling bag OEMs.
European and North American procurement managers require strict compliance with international chemical and safety benchmarks. Leading Chinese manufacturers certify their textiles against EU REACH regulations, RoHS environmental directives, and California Proposition 65. Products undergo rigorous testing for phthalates, heavy metals, azo dyes, and PFAS water-repellent coatings.
Modern B2B buyers rarely order standard catalog items. Successful manufacturers offer extensive OEM/ODM frameworks, supporting full custom mold development for trolley handles, custom debossed logo metal plates, branded interior jacquard linings, anti-theft RFID-blocking pockets, and modular internal organization dividers tailored to specific corporate needs.
Global brands are held accountable for their carbon footprint. Procurement managers actively seek factories utilizing recycled ocean plastic polymers, Global Recycled Standard (GRS)-certified rPET polyester, water-free dyeing processes, and factories audited under ISO14001 and BSCI (Business Social Compliance Initiative) standards.
Next-generation engineering features shaping the future of global travel gear and commercial luggage.
Transitioning from traditional dual-wheel inline skaters to double 360-degree silent TPU (Thermoplastic Polyurethane) spinner wheels with built-in steel ball bearings. These reduce rolling acoustic friction down to below 45 dB while enduring 30+ kilometers of continuous rough-asphalt testing.
Incorporating removable power bank trays with external USB-C fast-charging ports, smart Bluetooth proximity tracking tags, integrated digital weight scales built into the top handle, and TSA-approved biometric fingerprint locks for effortless border control.
Combining rigid drop-proof polycarbonate backings with expandable softside front compartments. This hybrid structure gives commercial travelers instant access to 16-inch laptops, documents, and tech gear without opening the main clothing compartment.
How modern rolling bag designs address specific commercial and industrial user scenarios.
Premium leather-trimmed rolling briefcases engineered specifically for executive travel. Equipped with shock-absorbing laptop sleeves, RFID-protected passport slots, and dimensions optimized to fit international airline overhead bin regulations (55 x 40 x 20 cm).
Heavy-duty wheeled tool and medical equipment bags featuring water-impermeable 1680D nylon exteriors, reinforced impact-resistant EVA bottoms, and custom modular dividers designed for field technicians, sales representatives, and medical staff carrying fragile equipment.
Industrial-grade wheeled flight bags engineered for extreme duty cycles (over 200 travel days per year). Featuring replaceable heavy-duty wheels, reinforced corner guards, anti-burst coil zippers, and quick-attach luggage straps for stacked bags.
Discover more customizable bags, totes, clutches, and travel gear manufactured for global distribution.



Essential technical and procurement insights for international wholesalers, retail buyers, and brand owners.
 Ripped Fashion